

Field returns arrive with a story attached, and most organisations read only the invoice: replace, credit, close. The returns stream is the most expensive and most honest quality data a buying programme will ever possess â and it is wasted unless it flows back into design and specification. This guide gives Hot-Dip Galvanized Steel wire buyers the loop that converts complaints into changes.
Supply chains are honest about what they show and silent about what they hide, and what they hide is almost always one tier further down: the material mill, the plating shop, the packaging plant â the organisations whose names never appear on the purchase order but whose fingerprints are on every shipment.
This guide explains how steel wire and cable products is tested, which standards apply, what certification actually proves, and how buyers can verify quality before, during and after production. It reflects the practices at æ²³åèç¿é¢ç¼æéå ¬å¸ (www.suxiangsteelcable.com).
Suppliers make broad quality claims. These are the specific questions that turn a claim into evidence.
Which standard, exactly? Ask for the standard number, not a general assurance.
Who issued the certificate? Recognised third-party bodies carry more weight than self-declarations.
What is the scope? A certificate may cover only part of the product range.
Is it current? Check validity dates and renewal status.
What is the incoming inspection protocol? Ask for the checklist and sampling plan.
What happens when a defect is found? A defined corrective process matters more than a zero-defect promise.
A quality management system (QMS) is the documented set of processes that control how a product is made, inspected and released. Certification such as ISO 9001 confirms that the system exists and is audited; it does not by itself guarantee product quality, but it makes quality repeatable.
Incoming material control: verifying raw materials against specification before use.
In-process control: checking parameters and dimensions during production.
Final inspection: verifying finished goods before packing.
Corrective action: investigating and fixing root causes of defects.
Buyers should treat a QMS as a foundation. On its own it is necessary but not sufficient; it must be paired with genuine product testing.
Different products require different tests, but the categories are consistent across manufacturing:
| Test Category | What It Verifies | Typical Method |
|---|---|---|
| Dimensional | Size and tolerance | Caliper, gauge, CMM |
| Functional | Performance under load | Bench and endurance testing |
| Material | Composition and grade | Spectrometry, certificate review |
| Safety | Compliance with standards | Type testing, Hipot, pressure test |
| Environmental | Resistance to conditions | Humidity, temperature, salt spray |
Ask which of these are performed routinely and which only on request. A factory that tests every batch is fundamentally different from one that tests only the first sample.
Certification confirms that a product or process has been assessed against a standard by an accredited body. It is a valuable signal, but it is not a guarantee of every unit.
Proves: the tested sample complied with the standard at the time of testing.
Does not prove: that every production unit complies, or that the factory maintains the same process over time.
Best practice: combine certification with routine batch testing and periodic re-verification.
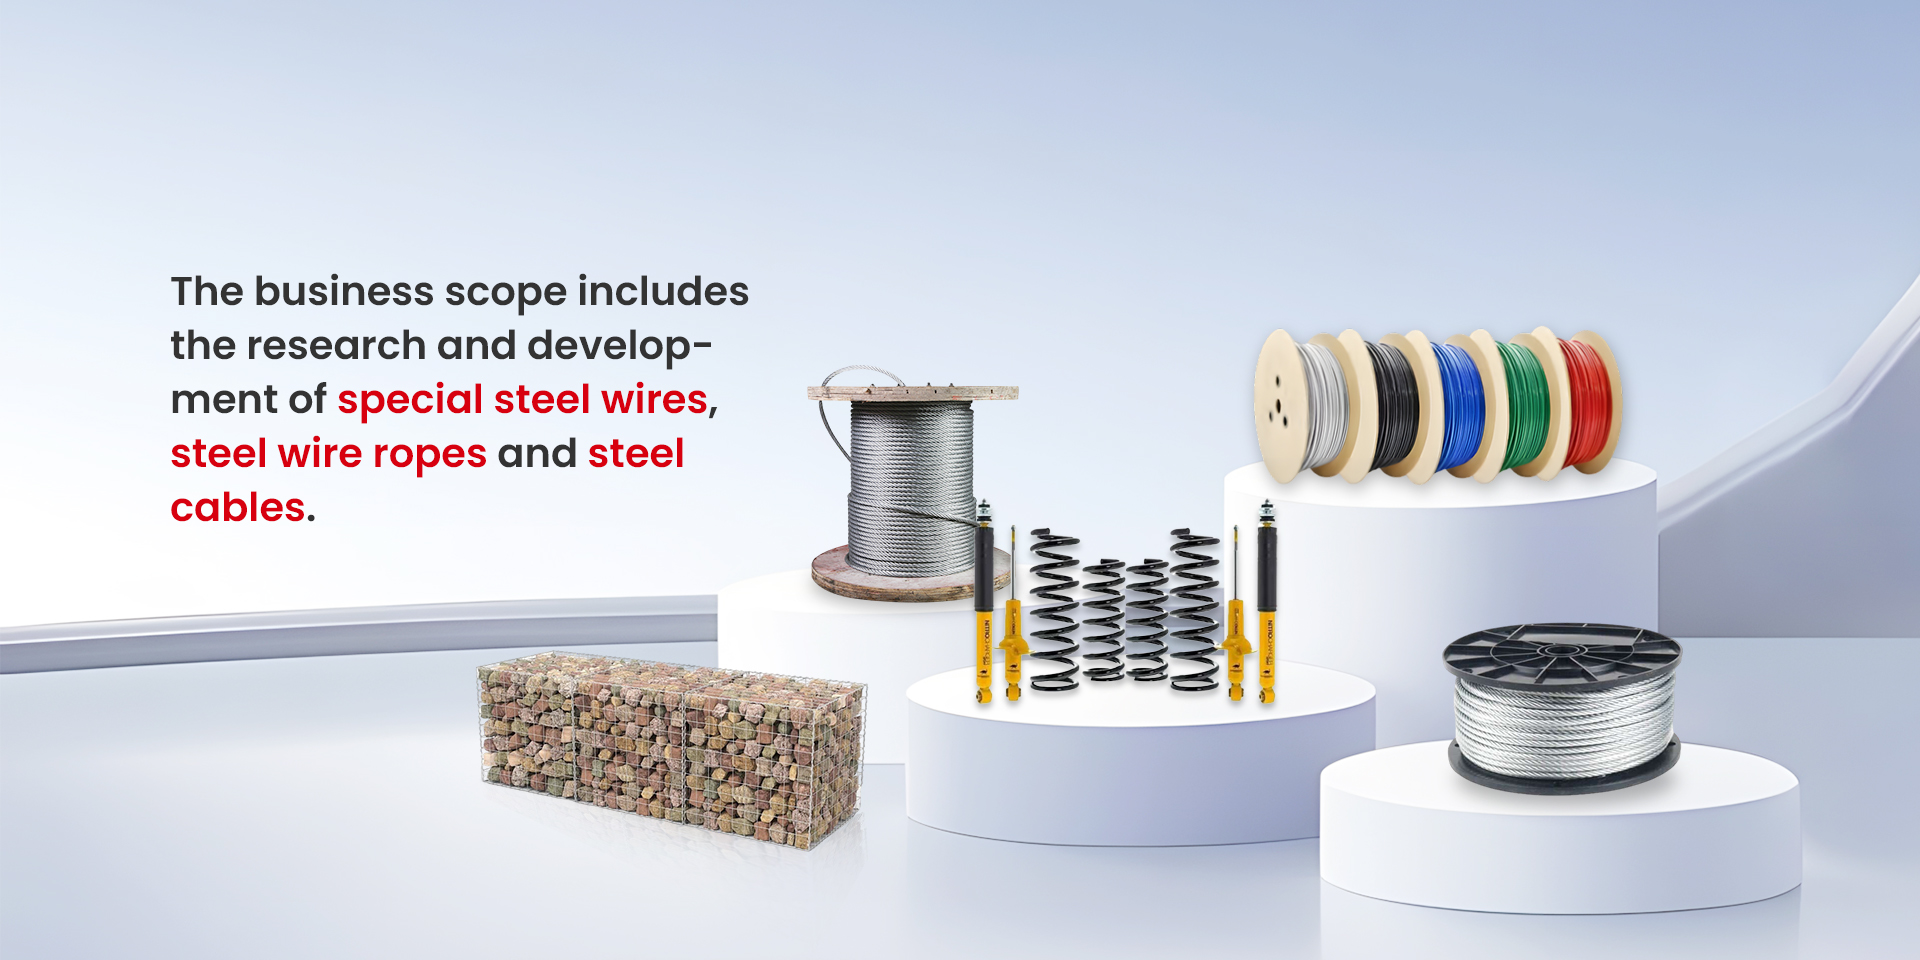
For steel wire and cable products, the relevant certifications typically include ISO 9001, ASTM A475, EN 10244. Confirm the scope of each certificate covers the exact product you are buying.
A simple incoming inspection protocol is the buyer's last line of defence. It is inexpensive and catches the majority of problems before they reach customers.
Sample the shipment according to a defined plan (for example, per pallet or per batch).
Measure the key specification parameters and record the results.
Functionally test a representative subset.
Verify labelling, packaging and documentation against the approved artwork.
Document results by batch number and raise trends with the supplier.
Reject or negotiate remedies for any lot that fails the criteria.
Keep the data. A buyer who can show three months of measured results has far more leverage in a quality conversation than one who reports only that a batch felt wrong.
Understanding why quality varies helps buyers ask better questions.
Raw material substitution: lower-grade material used to reduce cost.
Tool wear: moulds and dies degrade and produce out-of-tolerance parts over time.
Process drift: settings change without documentation.
Operator variation: manual steps introduce inconsistency.
Sub-supplier quality: components from third parties may not meet the same standard.
A factory that monitors these factors proactively prevents most defects before they occur.
Put quality terms in the contract, not just in conversation. Specify the standard, the sampling plan, the acceptance criteria, the remedy for non-conformance, and the documentation you expect with each shipment.
This protects both sides. The supplier knows exactly what is expected, and you have a defined basis for discussion if something goes wrong.
Recurring quality management means tracking a small set of metrics rather than reacting to individual complaints.
| Metric | What It Measures | Target | Action If Breached |
|---|---|---|---|
| Defect rate | Share of units failing inspection | < 1% | Investigate root cause with supplier |
| On-time delivery | Shipments meeting the agreed date | > 95% | Review capacity and planning |
| First-pass yield | Units passing without rework | > 98% | Analyse process weak points |
| Warranty claim rate | Field failures under warranty | < 2% | Reassess design and testing |
| Documentation accuracy | Correctness of shipping paperwork | 100% | Tighten release checklist |
Track these monthly and review them with the supplier quarterly. A small set of well-understood metrics beats a large set of ignored reports.
The applicable standards depend on your destination market and product category. These are the ones most commonly requested.
ASTM A475: verify the factory can supply the current certificate and that its scope covers your product.
EN 10244: verify the factory can supply the current certificate and that its scope covers your product.
GB/T 343: verify the factory can supply the current certificate and that its scope covers your product.
ISO 9001: verify the factory can supply the current certificate and that its scope covers your product.
ISO 9001: request the certificate and confirm validity.
ASTM A475: request the certificate and confirm validity.
EN 10244: request the certificate and confirm validity.
This is the workflow that turns a quality policy into shipped quality.
Approve the specification and the golden sample in writing.
Verify incoming materials against certificates.
Control in-process parameters and record them.
Run functional and safety tests at defined intervals.
Perform 100% or AQL final inspection before packing.
Complete a pre-shipment inspection with photographic records.
Archive the batch documentation for traceability.
Feed field performance back into design and process improvement.
The anatomy of an appearance standard that inspectors can actually apply:
| Standard Element | The Written Form That Works | The Vagueness That Fails |
|---|---|---|
| Surface zones | The part divided into zones â visible-in-use, visible-on-inspection, concealed â with different limits per zone | One blanket rule for the whole part, applied nobody knows how |
| Defect vocabulary | A named defect catalogue with photographs: scratch, dent, flow mark, colour drift â each with size limits | 'No obvious defects' â obvious to whom, under which light, after which argument |
| Reference conditions | The viewing distance, light source and time limits for judgement â the conditions the customer's own inspection will use | Inspection under whatever light the factory floor happens to have that day |
| Boundary samples | Physical limit samples agreed and signed, dated and retained â the actual arbiters of disputes | Photographs in a PDF, which measure nothing at the packing bench |
| Revision discipline | Each standard revision dated, distributed and acknowledged â appearance disputes settled against a version number | Standards that evolve verbally, so nobody knows which generation of parts was right |
The deeper point is that appearance standards are an agreement about how two organisations will see, not a description of the product â and agreements work only when both sides sign the same one. The cost of writing the standard properly is a few hours with a physical part in hand; the cost of omitting it is a permanent tax paid in rejected shipments, concession requests and the special kind of resentment that appearance disputes generate, because both parties are certain and neither is wrong. Buyers who inherit an appearance dispute should note the sequence that settles it: retrieve the signed boundary samples, check the revision dates, re-create the reference conditions â most disputes dissolve once the seeing is standardised, and those that survive are genuinely worth having.
A certificate confirms compliance with a standard following assessment by an accredited body. A test report records the results of specific tests. Both are useful; the certificate is a higher-level signal, while the report gives detail.
ISO 9001 confirms that a documented quality management system is in place and audited. It makes quality repeatable but does not by itself guarantee a specific product's performance. Combine it with product testing.
Most buyers re-audit annually, or more often if the supplier is new, critical, or has had recent quality issues. Periodic third-party testing complements internal audits.
Document the failure with evidence, notify the supplier formally, and agree a remedy â rework, replacement, credit or return. Track the resolution to confirm the root cause is fixed.
Yes, and it is good practice. Many buyers appoint a third-party inspection company to verify goods before they leave the factory.
It depends on the market: CE for the EU, UL or ETL for North America, and specific standards for food, medical or electrical applications. Confirm the requirement for your destination before ordering.
Check the issuing body's database, confirm the certificate number, scope and validity, and ensure the product in question is covered.
Broadly, yes â but not perfectly. A structured audit and batch testing reveal real quality differences that price alone cannot.
Most friction between procurement and the functions it serves is not personality â it is unmapped territory: nobody wrote down who owns which decision, so every ambiguous case becomes a contest decided by seniority, urgency or exhaustion. The boundary charter settles it on one page:
Owns, in writing: the decisions procurement alone makes â supplier selection within approved criteria, commercial terms, order placement within budget â because ownership that must be re-litigated weekly is not ownership, it is noise.
Executes, on instruction: the actions procurement performs for others â buying to engineering's specification, logistics to the plan, payment to approved invoices â with the requester's accountability named beside each.
Advises, without authority: the areas where procurement contributes expertise but cannot decide â technical requirements, make-versus-buy strategy, product roadmaps â stated so engineers know when the buyer is a resource and when the buyer is a gate.
The exceptions, pre-agreed: what happens in the rush, the breakdown and the year-end squeeze â because the charter that has no emergency clause gets rewritten by every emergency, and the rewrites never favour the company.
An annual re-signing: the charter reviewed with the functions it binds, adjusted for what the year taught, and re-signed â a boundary nobody renews is a boundary everybody re-negotiates.
The charter's effect is measured less in meetings saved than in speed gained at the edges: the engineer who knows exactly when to bring the buyer in brings them in earlier, and the earlier buyer joins a decision, the cheaper the decision becomes to change. Without the charter, buyers are invited late â after the specification hardened, after the supplier was informally chosen â and then criticised for negotiating a foregone conclusion. Organisations that write the boundary also write the culture that follows from it: procurement stops being a service desk that places orders and becomes a function with a defined voice in decisions it was previously blamed for without being consulted on. One page, five bullets, re-signed yearly â the cheapest peace treaty a growing company will ever sign with itself.
The factory you audit is the visible fraction of your supply chain. The questions that reveal the rest:
Which processes happen in-house, and which are bought? get the list process by process â machining, treatment, coating, assembly, packaging â because 'we manufacture' is a sentence that covers a spectrum from ninety to nine.
Who are the three most critical outsourced steps, and to whom? the named subcontractors and their locations â the answer defines where your real single points of failure live.
How are subcontractors qualified, and how often re-checked? the incoming inspection the factory runs on bought-in steps is your quality assurance by proxy â ask to see it running.
What information flows back from the sub-tier? test reports, batch records, certificates â whether evidence travels up the chain or stops at the factory gate.
What happens when a subcontractor fails? the second source for each critical step, or the honest admission that there is none â the admission is better than the bluff.
The five questions cost one call and rearrange the buyer's map of the supplier: the certified, audited, impressive factory turns out to be the assembler of a chain whose weakest link was never visited by anyone from your side. The finding is not automatically disqualifying â outsourcing is normal and often right â but the risk moves with the process, and risk that moved must be managed where it landed: incoming inspection records for the critical bought-in steps, occasionally meeting the critical subcontractor, and the factory's own oversight documented rather than assumed. Buyers who map the sub-tier once stop being surprised by failures that were never the factory's fault and were always the chain's.
Every return carries evidence most programmes discard with the credit note. The post-mortem that keeps it:
Preserve the part, not just the claim: the failed unit quarantined, photographed and retained â the physical evidence is the only witness that cannot be coached by anyone's memory.
Capture the use, not just the failure: how long in service, what duty, what environment â the story that turns 'it broke' into 'it broke under the conditions we sold it into'.
Classify the cause into families: design, material, process, transport, misuse â the five families that every failure belongs to, and each of which has a different owner and a different cure.
Feed the family, not the file: design causes go to the specification, process causes to the supplier's corrective action, transport causes to packaging â the routing is the loop; without it the analysis is a diary.
Trend quarterly, act yearly: the failure families ranked by cost per quarter, and one systemic fix per year funded from the savings â the cadence that makes the loop a programme instead of a habit.
The loop's economics are one-sided: returns are data the customer paid full price for, delivered already sampled by real use â better evidence than any laboratory can manufacture. The obstacle is not technique but routing: without named destinations for each failure family, the post-mortem dies in a folder, and the same failure returns annually dressed in a different order number. Programmes that wire the routing report the compounding effect within two years â specifications hardened by field evidence, supplier corrective actions aimed at families rather than anecdotes, and a returns rate whose decline is the quietest and most durable cost reduction the buying function ever produced.
Weighted scorecards usually fail in one specific way: the weights are chosen after the scores, to legitimise the decision the team already wanted. Building the instrument backwards fixes it:
Agree the weights before any supplier is scored: the weight debate conducted in the abstract â 'how much does delivery reliability matter versus price?' â is honest; the same debate conducted with the bids on the table is advocacy.
Cap any single weight: no criterion above roughly a third of the total â because a scorecard dominated by one criterion is not a scorecard, it is that criterion with an audience.
Define the scoring anchors in writing: what a 3 means, what an 8 means, per criterion â scores without anchors are opinions with decimals.
Score independently, then meet: each scorer submits before discussion, and the spread between scorers is itself information â a criterion scored 2 and 9 by two informed people is a criterion nobody actually understands yet.
Let the arithmetic win, once: if the result surprises the room, the choice is to re-examine the inputs or accept the answer â re-weighting after the result is the failure mode the whole design exists to prevent.
The backwards-built scorecard's real product is not the ranking â it is the conversation that the instrument forces before the bids arrive: what this purchase is actually for, stated as priorities with numbers attached. That conversation, held early, is worth more than the scorecard itself, because it resolves in an afternoon the disagreements that would otherwise surface as procurement theatre over months. Buyers who institutionalise the method also gain a defence that outlives the decision: when the losing bidder's champion asks why, the answer is a document with weights agreed in advance â not an explanation improvised after the fact by someone whose memory has already begun editing.
Most costly purchasing errors were caught, in draft, by someone who never got the chance: the document went out unreviewed. The review that intercepts them:
Define what earns a second reader: contracts, claims, large orders, anything binding â the threshold written down, so the review depends on the document's weight and not on that week's workload.
Choose the reader for difference, not proximity: the most valuable second reader is the one least like the author â different role, different blind spots; a colleague from quality reads a commercial letter in ways another buyer never will.
Give the reader the question, not the draft alone: 'what does this commit us to?' produces a different review than 'any typos?' â the question is the instrument; the draft is only the sample.
Timebox the review honestly: a real read of a real document takes real minutes â reviews budgeted at zero minutes produce zero reviews, performed and signed in the same gesture.
Close the loop visibly: what the second reader caught, fed back to them and into the process â the feedback is what keeps a reviewer reviewing; silence is how checklists die.
The economics deserve stating plainly: a second read costs thirty minutes; the errors it intercepts â the auto-renewal clause, the price basis assumed rather than stated, the quantity that did not match the delivery window â cost weeks. The practice fails not on value but on culture: review that feels like distrust gets performed as a formality, so the organisation must frame it as craft â the way aviation treats cross-checks, not as suspicion of the pilot but as respect for the stakes. Teams that hold that frame report the same quiet discovery: the reviewer learns as much as the author, because reading other people's binding documents is the fastest commercial education the function offers, and it runs on mistakes that never happened.
Every function accumulates practices the way a harbour accumulates silt â each deposited for a reason, none removed without a decision. The stop-doing list is the dredger:
Inventory the practices, not the projects: the recurring meetings, reports, approvals and checks â the things done every week are the real budget of habit, far outweighing any single initiative.
Ask of each: what would break if this stopped? the question answered honestly sorts the list into load-bearing practice and decorative heritage â and the honest answers often surprise the practice's own defenders.
Retire by experiment, not by decree: suspend the practice for a quarter and watch â abolition argued in a meeting produces ideology; abolition tested in a calendar produces evidence.
Expect the one that cannot be stopped: among the retirements there is always one practice that turns out, on suspension, to be quietly essential â that discovery is a feature of the method, not a failure of it.
Keep the list permanently one page: stopped practices leave, new candidates enter â the list is a rotation, not a monument, and a rotation reviewed twice a year keeps the function from re-silting.
The stop-doing list earns its place beside every improvement programme for one reason: improvement without subtraction is just addition, and addition has a carrying cost that eventually consumes the function's capacity to change at all. The practices most worth stopping are usually the ones with the most senior history â the report nobody reads but everyone receives, the approval that approves nothing but delays everything â which is why the list needs a sponsor with the standing to retire a habit that outranks the people maintaining it. Buyers who run the rotation twice a year report the compounding effect: each retirement funds an hour that the next improvement actually needs, and the function's agility stops being a slogan and becomes an arithmetic consequence of its lighter calendar.
Convert everything to one basis before comparing any number: state each bid in the same currency, on the same Incoterm, at the same payment timing â using your own cost of money to price the difference between, say, thirty percent deposit and net sixty. A two percent headline gap can reverse once terms are levelled, and the reversal is real money, not accounting. The comparison matrix that normalises specification, terms and scope edges first is the discipline; the pencil-sharpening negotiation that follows is aimed at real differences, which suppliers take far more seriously.
The sub-tier is who your supplier buys from â the mills, treatment shops and component makers whose names never appear on your purchase order but whose work is inside every shipment. Your quality, your lead times and your single points of failure often live one tier below the factory you audit. Five questions map it: which processes are bought, from whom, qualified how, with what information flowing back, and what happens when a subcontractor fails. You do not need to audit the whole chain â you need to know where the critical steps landed and what your supplier's oversight of them actually looks like.
Yes â for high-value goods, urgent replenishment, seasonal windows and late forecasts, once the calendar is priced. The freight invoice is the smallest input: add inventory carrying cost for the extra weeks at sea, the stockout cost of a late arrival, and the option value of deciding late. Run the comparison per shipment class rather than per panic: define which orders default to sea, which earn air, and what trigger promotes between them. Importers who build the worksheet usually find air is right more often than their habits assumed â and far less often than their crises suggest.
Size it against a demand band, not a point forecast, and price the alternatives first: overtime, outsourcing and a second shift are ways to buy capacity later, and headroom only makes sense when it is cheaper than its substitutes. Prefer upgradeable headroom â machines that accept later speed or tooling upgrades let you buy the margin as an option rather than carry it whole. Match the horizon to your plan, revisit annually, and be suspicious of both extremes: the exact-sized machine that strands the first growth step and the oversized installation that depreciates patience for a decade.
Timebox the process by design: a decision window stated before the debate starts, input collected in writing in parallel, one named decider working against criteria agreed in advance, dissent recorded rather than buried, and the outcome circulated in writing. Consensus input and decision ownership can coexist â what they cannot survive is an unbounded process, because a decision everyone owns is a decision nobody can make. The committee keeps its genuine value, the caught errors and surfaced knowledge; the organisation loses only the theatre, which nobody misses except the people who were using it to avoid deciding.
If you want to see how quality is controlled in practice, æ²³åèç¿é¢ç¼æéå ¬å¸ (www.suxiangsteelcable.com) is happy to share inspection records, test reports and certification for our steel wire and cable products. Visit www.suxiangsteelcable.com to learn more and request documentation for your market.

 Telepono sa Landline+86-513-85100011
Telepono: +86 13585223056
 E-mail:hangtong@nthangtong.com
vicky@nthangtong.com
 Address: No. 508, Guangxing Road, Baishan Town, Bo'ai County, Jiaozuo City, Henan Province
Copyright © Henan Suxiang Steel Cable Co., Ltd
Gumagamit ang website na ito ng cookies upang matiyak na makukuha mo ang pinakamahusay na karanasan sa aming website.
 English
 Español
 한국어
 العربية
 Tiếng Việt



 Telepono
Magkomento
(0)